Phosphate ester hydraulic fluids are used where fire resistance is critical, including power generation, aviation, steel production, furnaces, and die-casting equipment.
These fluids can provide valuable safety benefits, but they are chemically demanding. Many elastomers, coatings, adhesives, paints, and sealing materials used in ordinary hydraulic systems are not suitable for phosphate ester exposure. Installing a standard oil-service hose without verifying the tube compound can lead to swelling, softening, loss of strength, leakage, or premature assembly failure.
Selecting a phosphate ester hydraulic hose therefore requires a system-level compatibility review. The fluid name, hose tube, reinforcement, cover, fittings, seals, temperature, pressure, and maintenance materials must all be considered together.
What Are Phosphate Ester Hydraulic Fluids?
Phosphate esters are synthetic fire-resistant fluids. In hydraulic-fluid classification systems, they are commonly associated with the HFDR category. Their chemistry and fire behavior differ from mineral oils, water-glycol fluids, and oil-water emulsions.
The exact formulation still matters. Different products may use different additives and may be designed for turbine control, industrial hydraulics, aviation, or other specialized duties. Compatibility should be confirmed for the named product rather than inferred from the words phosphate ester alone.
The fluid supplier’s technical data and compatibility guidance are essential starting points. A hydraulic hose materials overview can help buyers understand how tubes, reinforcement, and covers work, but final approval must be tied to the actual fluid and operating conditions.
Why Standard Oil-Resistant Tubes May Fail
Oil resistance and phosphate ester resistance are different properties. A tube designed for petroleum hydraulic oil may absorb phosphate ester fluid, causing it to swell and soften. The material can lose tensile strength, change dimensions, or separate from surrounding layers.
In other cases, the fluid may extract ingredients from the elastomer, leading to shrinkage, hardening, or cracking. The reaction can affect how the hose seals against the fitting insert and how the tube behaves during pressure cycling.
Heat accelerates many chemical reactions. A hose that survives a short bench exposure at room temperature may not provide an acceptable service life at the system’s maximum temperature. Pressure impulses and flexing add mechanical stress to any chemically weakened material.
Tube Materials Commonly Considered
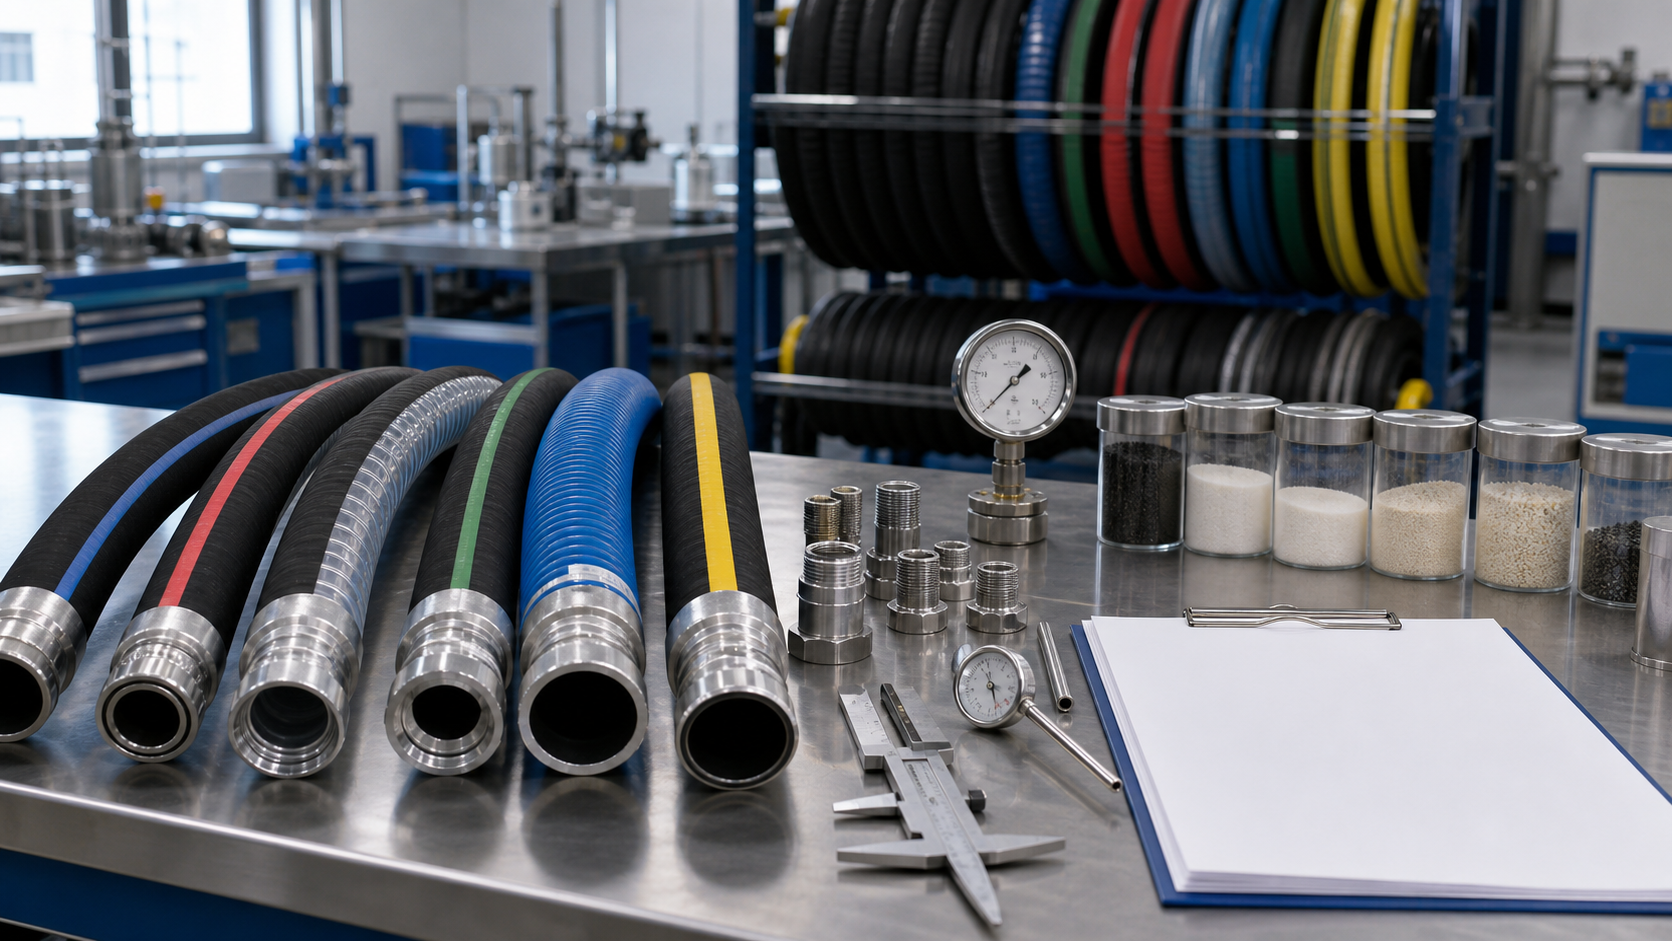
There is no single tube material that is best for every phosphate ester system. Several material families may be evaluated depending on the application.
EPDM-based compounds
EPDM is often considered for phosphate ester and other fire-resistant fluid applications because selected formulations can provide suitable chemical resistance. However, EPDM compounds vary, and not every EPDM hose is a high-pressure hydraulic hose.
The tube must be part of a complete construction with the required reinforcement, temperature rating, cover, and compatible fitting system. A low-pressure EPDM industrial hose cannot be substituted for a high-pressure hydraulic assembly simply because the base elastomer is compatible.
EPDM also has poor compatibility with many petroleum oils. This becomes important during system conversion, maintenance, and accidental cross-contamination.
Butyl-based compounds
Selected butyl or related compounds may be used with certain phosphate ester fluids. They can offer useful chemical and permeation characteristics, but again, the specific formulation and complete hose design must be approved.
Buyers should request evidence for fluid exposure at relevant temperature rather than relying only on a generic elastomer chart.
PTFE tubes
PTFE hydraulic hose is frequently considered for aggressive fluids because PTFE has broad chemical resistance and a wide temperature capability. It can be a strong candidate for phosphate ester service when the pressure, reinforcement, fittings, motion, conductivity, and permeation requirements are properly addressed.
PTFE hose behaves differently from rubber hose. It may have a larger minimum bend radius, lower resistance to repeated bending at one concentrated point, and specific requirements for braid and fittings. Corrugated constructions can improve flexibility, while smooth-bore constructions may provide easier cleaning and lower flow resistance.
PTFE should be selected as a complete engineered assembly, not as tube material alone.
Use Compatibility Charts as Screening Tools
A fluid compatibility guide can eliminate clearly unsuitable material families and identify candidates for further review. It cannot capture every fluid brand, additive package, concentration, temperature, or duty cycle.
Compatibility symbols such as excellent, good, conditional, or not recommended also need context. “Good” at room temperature may not mean acceptable at 120°C. A material may show limited swelling but experience changes in strength that matter under high pressure.
For critical service, ask for test conditions behind the rating. Useful information includes exposure time, temperature, changes in volume and hardness, tensile retention, and visual condition.
Pressure and Impulse Requirements
After identifying a compatible tube, confirm the mechanical performance of the complete hose. The working-pressure rating must cover the maximum pressure for the selected size. Burst pressure is not the normal operating limit.
Systems controlling turbines, furnaces, presses, or flight equipment may experience frequent pressure cycles and rapid transients. Impulse capability can be as important as static pressure. Reinforcement should be chosen according to the duty rather than oversized or undersized based only on a familiar hose standard.
The hose should also maintain pressure capability at the maximum allowed temperature. If the manufacturer applies temperature derating, use the reduced value in the system design.
Fittings and Sealing Materials
The fitting insert, ferrule, plating, O-rings, flange seals, and thread sealants must be compatible with the fluid. A suitable hose tube does not protect an incompatible O-ring.
Many standard hydraulic seals are selected for mineral oil. Phosphate ester systems may require different elastomers. Follow the fluid and component suppliers’ recommendations rather than choosing by color or appearance.
Crimp dimensions are specific to the hose and fitting combination. Do not attach a familiar fitting to a specialty hose without an approved assembly procedure. The wrong insert profile or crimp diameter can damage the tube or reduce fitting retention.
Avoid Mineral-Oil Cross-Contamination
Converting an existing system can be challenging because phosphate ester-compatible materials may not tolerate residual petroleum oil, while the new fluid’s performance may be affected by contamination.
Hoses used with the previous fluid should be evaluated carefully. Reusing them can introduce contamination and may leave an incompatible tube in service. New assemblies should be capped, stored cleanly, and installed after the system is prepared.
Do not use an unapproved solvent for flushing. Cleaning agents can attack seals, tube materials, adhesives, or reservoir coatings and may be difficult to remove completely.
Temperature Management
Phosphate ester systems are often associated with high-temperature equipment, but the fluid and hose still have defined operating limits. Measure temperature at representative points during maximum load, not only at the reservoir during idle operation.
Route hoses away from direct radiant heat and hot surfaces. Use guards, insulation, or sleeves where necessary. Avoid enclosing the assembly so tightly that heat cannot dissipate or inspection becomes impossible.
Cold conditions should also be reviewed. Fluid viscosity, hose flexibility, and pump inlet performance can change during start-up. The complete temperature range belongs in the purchasing specification.
Testing a Proposed Hose Construction
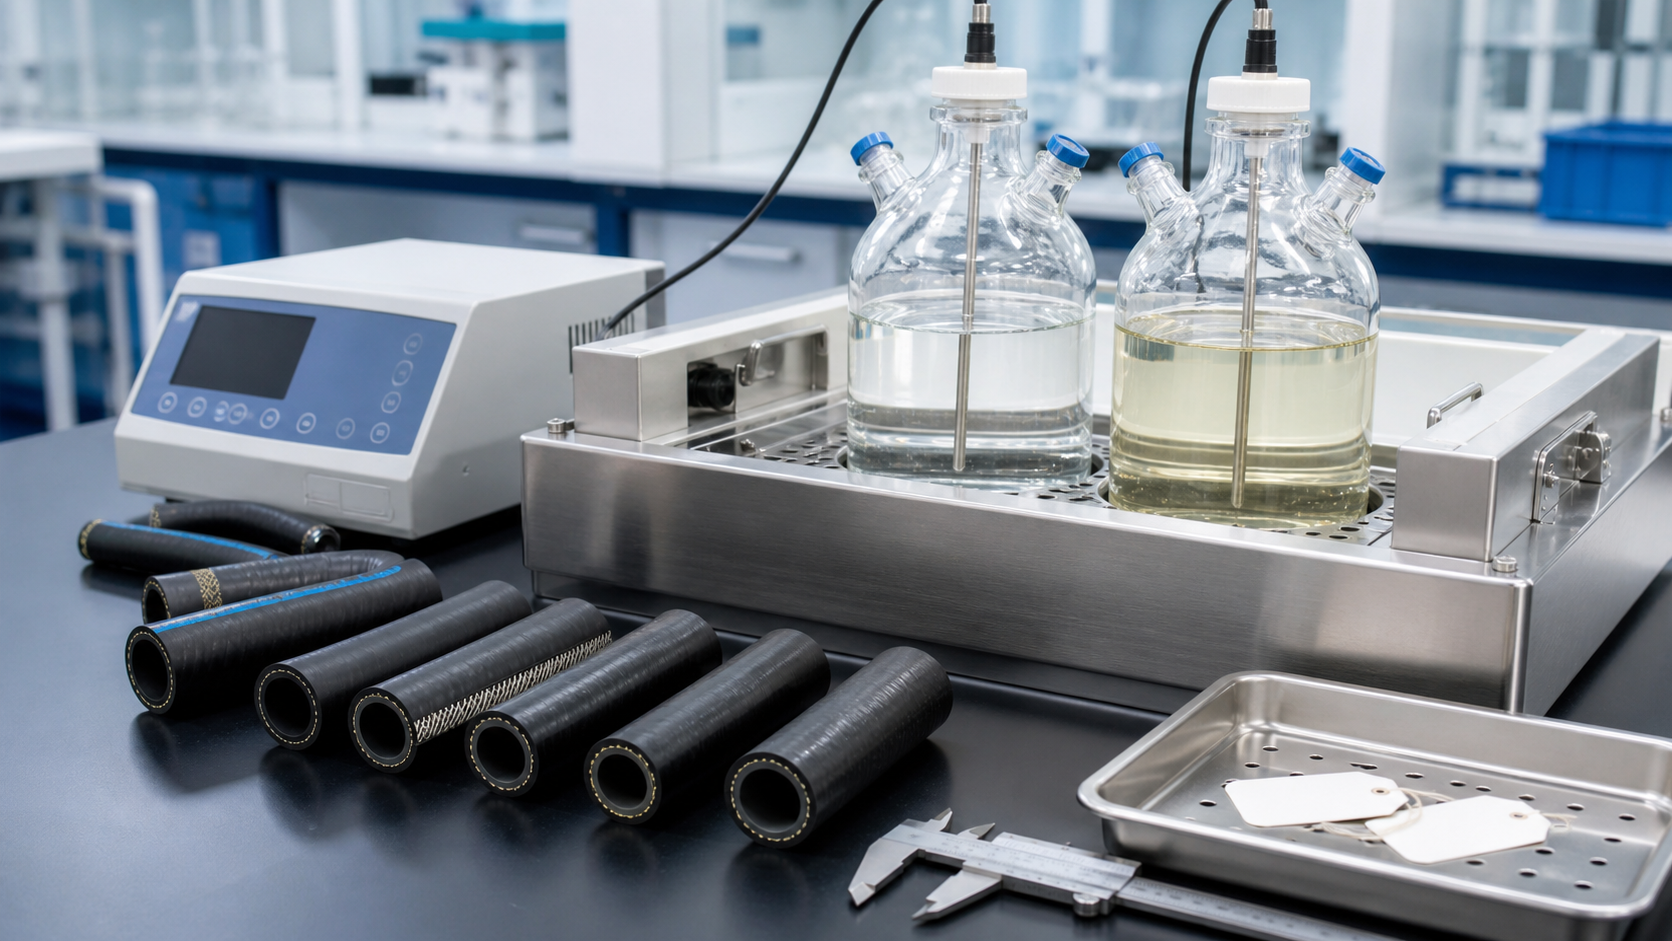
When direct approval for the fluid is unavailable, a formal test program may be necessary. A useful program can include:
- Controlled fluid immersion at representative temperature
- Measurement of volume and hardness change
- Tensile and elongation retention
- Visual checks for swelling, cracking, tackiness, or blistering
- Tube-to-reinforcement adhesion evaluation
- Pressure and impulse testing after exposure
- Fitting-retention checks
- A monitored field trial in representative equipment
Use the actual fluid, not a generic substitute, and review results before production approval.
Information to Put on the Purchase Specification
For OEM or plant purchasing, document:
- Exact phosphate ester fluid brand and product
- Approved hose manufacturer and construction
- Hose size and working-pressure requirement
- Temperature range
- Reinforcement and cover requirements
- Fitting series, material, and seal type
- Assembly length and fitting orientation
- Cleaning and capping standard
- Required tests and certificates
- Marking or layline requirements
- Inspection and replacement criteria
This prevents future buyers from ordering a general-purpose hose with the same dimensions but the wrong tube material.
Inspection in Service
Inspect specialty-fluid hose assemblies for leakage, cover softening, blistering, cracking, fitting movement, discoloration, and loss of flexibility. Pay close attention to areas near heat sources, clamps, guards, and fittings.
A small surface change can be an early warning of fluid exposure or chemical incompatibility. If one assembly shows unusual deterioration, inspect other hoses from the same specification and review fluid condition before installing another identical replacement.
Maintain records of installation date, operating hours, fluid changes, inspection results, and removed-hose findings. This information helps refine replacement intervals and detect systemic problems.
Conclusion
Phosphate ester fluids require hose materials selected specifically for their chemistry. Selected EPDM, butyl, PTFE, or other specialty constructions may be suitable only when the complete assembly is approved for the exact fluid, temperature, pressure, and duty. Compatibility charts are useful for screening; documented testing and supplier approval are needed for critical service. Put these requirements in the purchasing specification to preserve fire resistance while reducing avoidable failures.